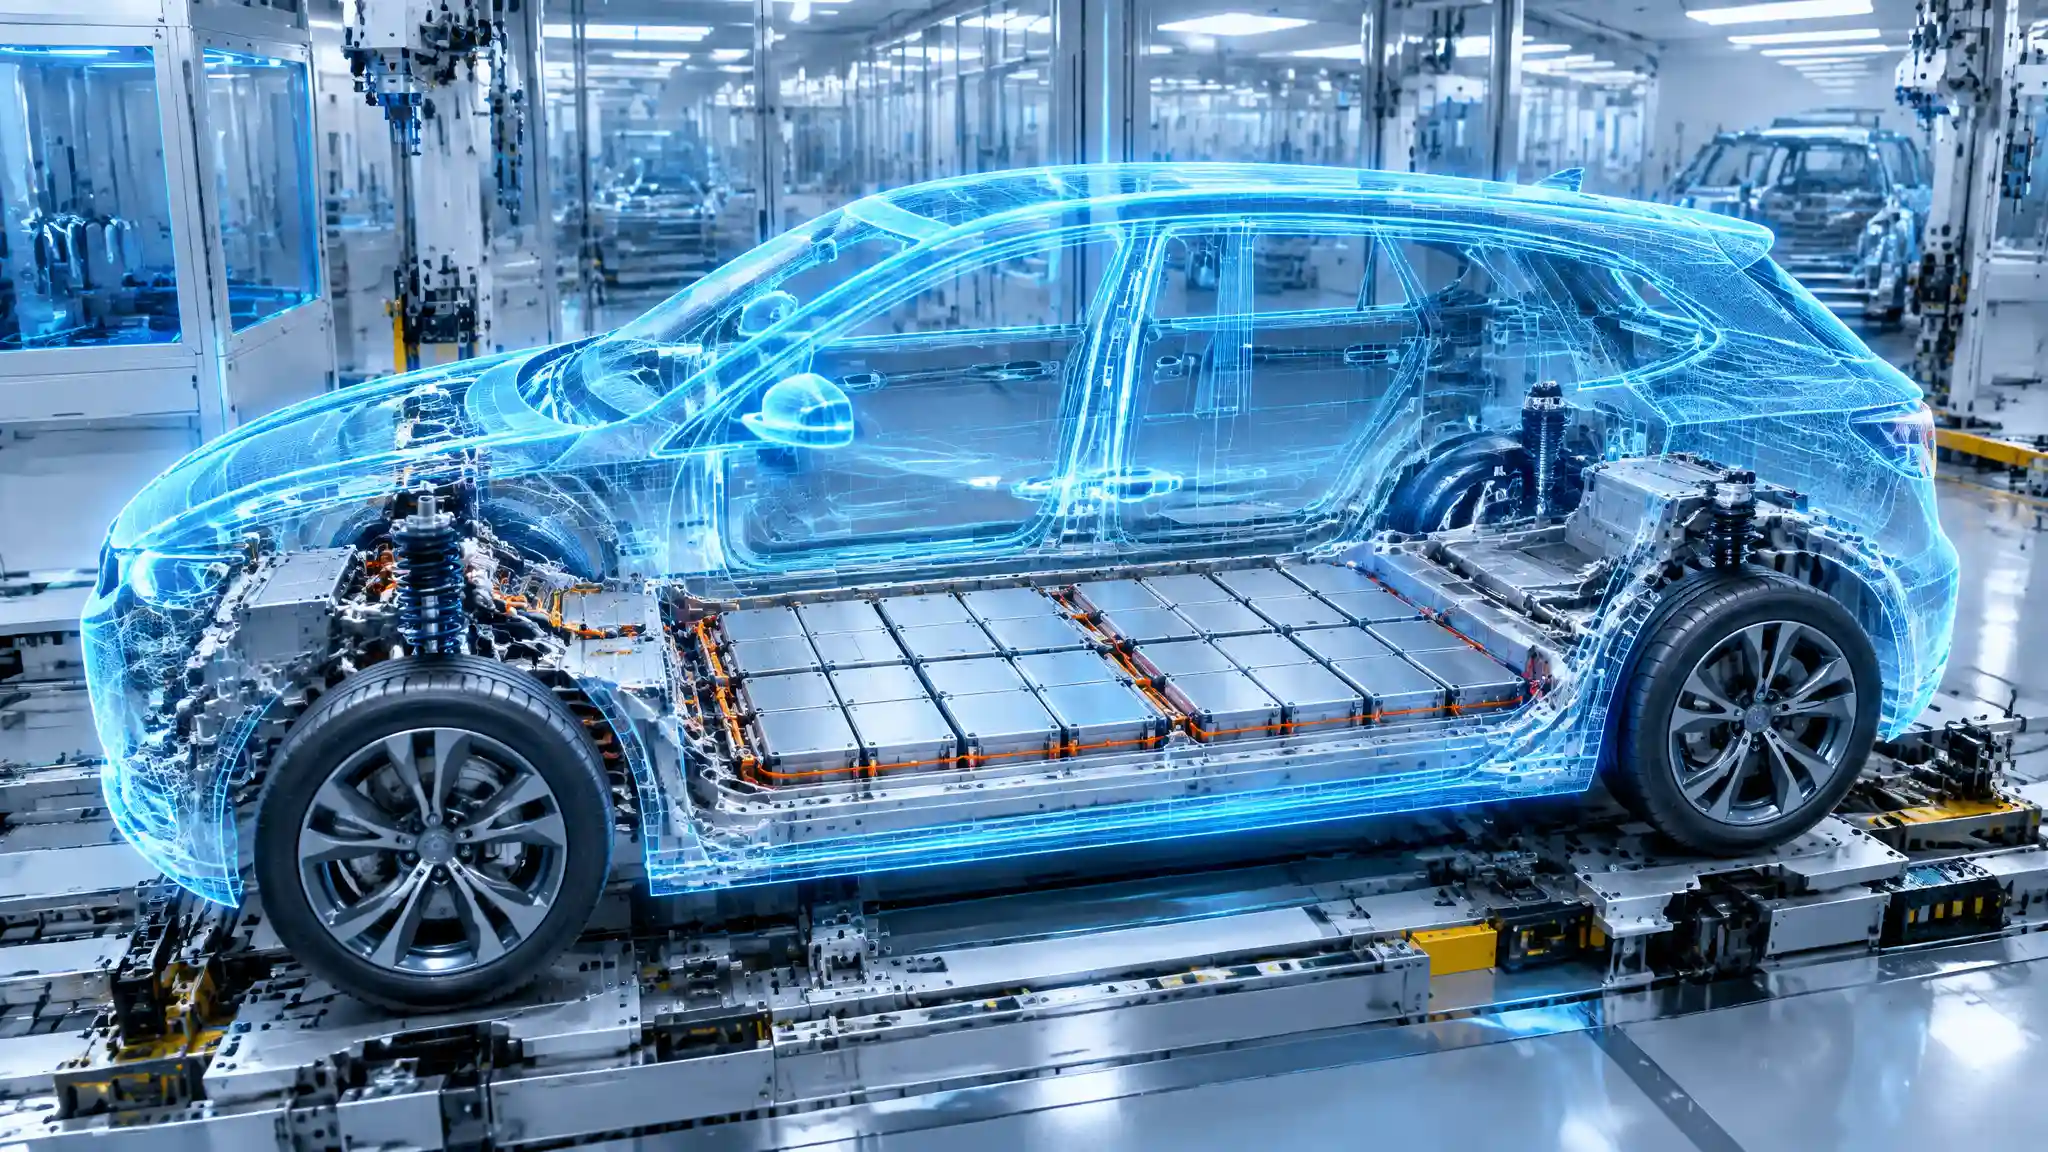
The floorpan sets the limit on range. In a sub-£30,000 hatchback, the battery has to supply the energy, carry structural load and meet Rules of Origin, all within one slab between the axles, and without pushing the H-point up into crossover territory.
This Built in Britain instalment sets out the battery specification for our reference hatchback. The chemistry is sodium-ion. The packaging is Cell-to-Pack. Cells are converted in Coventry. Every figure below comes from the reference framework's engineering and cost model.
Pack specification at a glance
- Chemistry: pure sodium-ion, "Sovereign Cell" architecture, at 200 Wh/kg cell level. No LFP, no nickel-based lithium-ion, no hybrid blend.
- Gross energy: 55 kWh.
- Active cell mass: 275 kg.
- Cell-to-Pack efficiency: 76% (cell mass ÷ pack mass).
- Finished structural pack mass: 361.8 kg.
- Pack-level specific energy: ≈152 Wh/kg.
- Height envelope: 110–130 mm, including enclosure, cooling plate and underbody protection.
- Factory-gate pack cost: £2,258, or ≈£41.1/kWh.
The mass budget: why 76% is the number that matters
The cell figure is fixed: 55 kWh at 200 Wh/kg gives exactly 275 kg of active cells. The only open variable is how much non-cell mass the pack adds around them.
At 76% Cell-to-Pack efficiency:
- 275 kg ÷ 0.76 = 361.8 kg finished pack.
- Non-cell mass (enclosure, cooling plate, busbars, BMS, thermal interface material, adhesive, underbody shield, sealing): 86.8 kg.
- Pack-level density: 55,000 Wh ÷ 361.8 kg = 152 Wh/kg.
Compare this with a conventional module-based layout at around 60% efficiency. The same 275 kg of cells would need a pack of roughly 458 kg, adding about 96 kg of parasitic mass. That penalty feeds straight into suspension rates, tyre sizing, brake specification and, in the end, into Wh/mile.
At 200 Wh/kg, sodium-ion cannot afford a module layer. Cell-to-Pack efficiency is what makes the chemistry workable in a hatchback.
How the 76% is achieved
- Large-format prismatic cells laid directly into the tray. No module housings, end plates or module-level harnesses.
- Structural adhesive bonding. The cell stack carries shear load between the tray and the lid, so the enclosure can use thinner sections.
- An integrated cooling plate as the tray floor. One part does two jobs: thermal management and structure.
- Laminated busbars and a distributed BMS. Removing conventional harness runs cuts both mass and height.
Sodium-ion battery packaging in 110–130 mm
The height target is non-negotiable. Each extra 10 mm of pack height raises the floor, cuts rear headroom and pushes the roofline up, which costs drag. Above about 130 mm, the car stops being a hatchback.
Sodium-ion's lower volumetric density compared with nickel-based lithium-ion makes this harder. There are three answers:
- Use the full footprint. The pack runs sill to sill and axle to axle. The crash load path goes around the pack through the sills, not through it.
- Put the cells on their side. Orient the prismatic cells so the thinnest dimension sets pack height, with a single cell layer and no stacking.
- Use a thin thermal system. Sodium-ion has a wide operating window and keeps its capacity in the cold, so the cooling plate can be sized for fast-charge heat rejection alone. Low-temperature performance needs no extra margin.
The result is a single-layer, fully structural slab. Sodium-ion battery packaging at this height depends on getting every millimetre of the stack-up right: underbody shield, tray, cooling plate, thermal interface material, cell, busbar and lid.
Sourcing: importing IP, not cells
The supply model is the core of sub-£30k UK EV manufacturing. The programme does not import finished cells. It imports chemistry.
CATL LRS: licensing, royalty and services
- Cell chemistry IP, process know-how and cathode precursors come through CATL's LRS (Licensing, Royalty, and Services) platform.
- Precursors arrive as bulk powders, not finished cells. That is lower-value, denser freight with a simpler dangerous-goods classification.
- The value-adding steps take place in the UK: electrode manufacture, cell assembly, formation and pack integration.
The domestic feedstock loop
- Sodium carbonate: from Cheshire, supplied by Tata Chemicals Europe. It is the sodium source for cathode synthesis and electrolyte salt production.
- Hard carbon anode: made from bio-waste pitch sourced from Scottish and Humberside streams, then carbonised into disordered hard carbon. Sodium-ion does not use graphite, so there is no exposure to imported graphite.
- Current collectors: copper-free aluminium foil on both electrodes, developed through Alvance and Innoval. Sodium does not alloy with aluminium at anode potentials, so copper is not needed anywhere in the cell.
Going copper-free matters beyond the cost per tonne. Aluminium on both sides means the cells can be stored and shipped at 0 V without dissolving the current collector. That simplifies logistics between the cell plant and the pack line.
Final conversion: UKBIC, Coventry
Electrode coating, cell assembly and formation take place at the UK Battery Industrialisation Centre in Coventry. From there, cells go straight into the Cell-to-Pack line: cell loading, adhesive bonding, busbar integration, end-of-line inspection and final assembly.
UKBIC dry room production: the gating constraint
The main risk to production volume is moisture, not cell supply.
Sodium-ion active layers are strongly hygroscopic.
- Layered-oxide cathodes react with atmospheric H₂O and CO₂ and form surface NaOH and Na₂CO₃. The result is slurry gelation during mixing, poor adhesion to the coating and gas generation during formation and cycling.
- Hard carbon, with its high surface area and open porosity, adsorbs water easily. That water drives first-cycle irreversible capacity loss and consumes electrolyte.
- Electrolyte salts hydrolyse in the presence of moisture and form acidic by-products that attack the interfaces.
So UKBIC dry room production runs to a strict atmospheric specification:
- Dew point below −40°C throughout the coating hall.
- A hyper-dry, inert nitrogen blanket over exposed electrode surfaces, to exclude both moisture and CO₂.
- Tight control of temperature and oxygen levels, with airlocked material transfer between zones.
This is a production gate, not just a quality target. Dehumidification capacity, air-change rate and airlock throughput set the maximum line speed. Any excursion above the dew-point limit means quarantining work in progress. Dry-room energy use is also a significant, continuous overhead, and it is included in the loaded pack cost below.
Economics: a £2,258 pack
Cost build-up
- Global raw cell chemical contract: $38/kWh.
- For 55 kWh: 55 × $38 = $2,090.
- At $1.30 to £1: $2,090 ÷ 1.30 = £1,608.
- Conversion and enclosure overhead: £650. This covers UKBIC conversion and dry-room running costs, the structural enclosure, cooling plate, BMS and pack integration.
- Fully loaded factory-gate pack cost: £1,608 + £650 = £2,258, or about £41.1/kWh.
The chemistry accounts for 71% of the pack cost. Conversion and enclosure account for 29%. Because the cost is weighted towards chemistry, further gains in Cell-to-Pack efficiency and dry-room productivity go straight to the bottom line.
9.0% of the build: breathing room for the bill of materials
- Net manufacturing budget: £25,000 per vehicle.
- Battery share: £2,258 ÷ £25,000 = 9.0%.
- Remaining for everything else: £22,742.
In early nickel-based EVs, the battery often took a third or more of the bill of materials. At 9.0%, the pack stops dictating how the rest of the car is specified. That freed budget goes where buyers notice it and where the platform needs it:
- Body-in-white and crash structure. Sill-based load paths strong enough to protect a 361.8 kg structural pack, without resorting to exotic materials.
- Thermal system. A heat pump and battery preconditioning as standard, not as options.
- Power electronics. An efficient inverter and on-board charger that turn 152 Wh/kg at pack level into competitive Wh/mile.
- Interior and safety systems. Enough specification to compete on showroom perception, not just on price.
- Margin and contingency. A buffer against swings in commodity prices and exchange rates. A 10% move in the dollar shifts pack cost by only about £160.
That breathing room is what turns a sub-£30k retail price from an aspiration into a viable business case.
Rules of Origin: post-2027 compliance
From 1 January 2027, the UK–EU Trade and Cooperation Agreement caps non-originating materials in an EV at 45% of ex-works price. A vehicle that fails pays the 10% tariff on every cross-border sale.
The LRS model is built for this rule:
- Imported content is limited to licensed IP and precursor powders, the lowest-value stage of the cell supply chain.
- Sodium carbonate, hard carbon, aluminium foil, cell conversion and pack assembly are all UK-originating.
- The whole pack accounts for only 9.0% of vehicle cost, and the imported chemistry contract is just £1,608 of a £25,000 build (about 6.4%). Even the most conservative treatment of the imported precursors keeps their contribution well inside the 45% cap.
The outcome is full compliance with the post-2027 TCA 45% threshold, with tariff-free access to the EU and no dependence on finished-cell imports.
Engineering summary
- 55 kWh sodium-ion, 200 Wh/kg at cell level.
- 275 kg of cells, 361.8 kg pack, 76% Cell-to-Pack efficiency, 152 Wh/kg at pack level.
- 110–130 mm single-layer structural slab.
- CATL LRS precursors plus Cheshire soda ash, bio-waste hard carbon and copper-free aluminium foil.
- Cell conversion at UKBIC Coventry, with the dry room held below −40°C dew point under nitrogen.
- £2,258 pack ($38/kWh chemistry at $1.30/£1 plus £650 conversion), 9.0% of a £25,000 build, TCA-compliant after 2027.
The battery bottleneck is solved through integration, not chemistry alone. Sodium-ion provides the cost floor. Cell-to-Pack recovers the mass. Coventry provides the origin.
Next in Built in Britain: Read Part 2: The Inverter Innovation and Silicon Carbide Tech Lowering EV Costs.